Extruded vs Die Cast Aluminium Heat Sinks: How to Choose
Extrusion and die casting are both core aluminium processes — and choosing the wrong one costs you money on every unit. A practical decision framework from a factory that runs both.
We run both processes under one roof, so we have no reason to steer you toward either one. Here is the honest framework.
The core difference
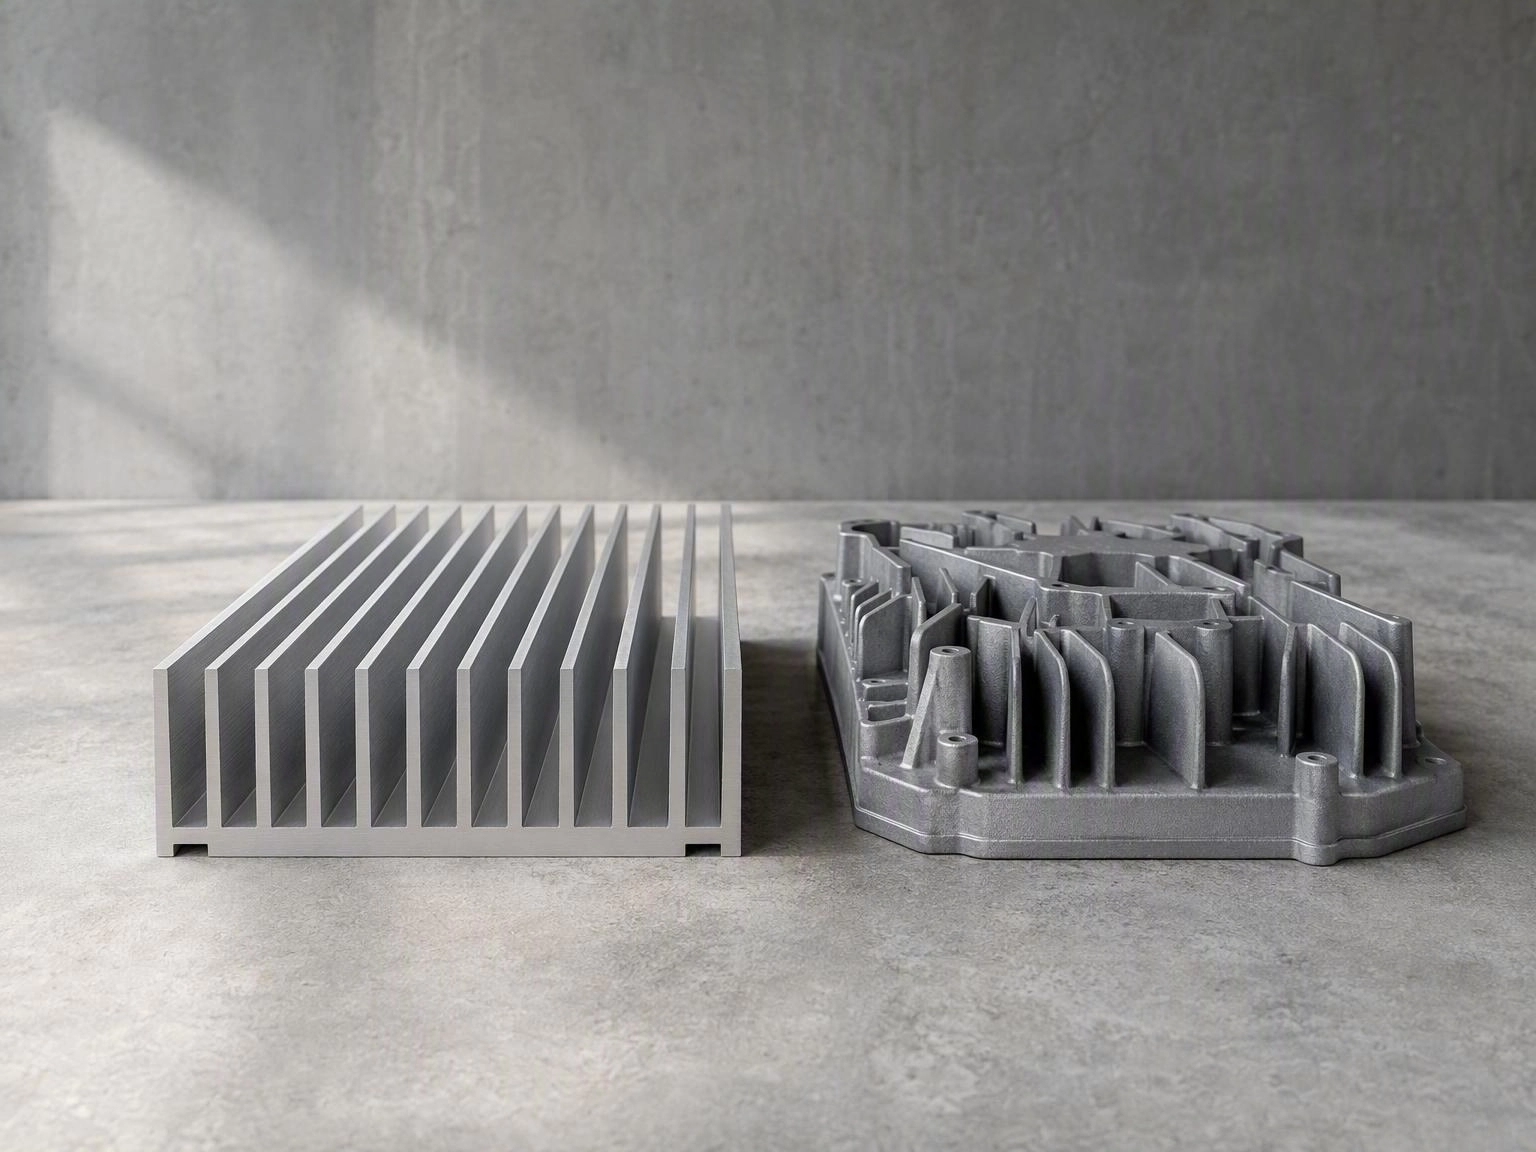
Extrusion forces heated aluminium billet through a die, producing a continuous profile of constant cross-section. You then cut it to length and machine the details.
Die casting injects molten aluminium into a steel mould, producing a near-net-shape part with complex three-dimensional geometry in a single shot.
Extrusion is a 2.5D process — the cross-section is arbitrary, the length is straight. Die casting is fully 3D, but with process constraints on wall thickness, draft angles and internal cavity complexity.
Cost structure
This is where the two diverge most sharply.
| Cost factor | Extrusion | Die casting |
|---|---|---|
| Tooling cost | Low to moderate | High |
| Tooling lead time | Short | Longer |
| Unit cost at low volume | Low | High |
| Unit cost at high volume | Low | Low |
| Machining required | Often significant | Often minimal |
| Break-even volume | Very low | Moderate to high |
Extrusion tooling is comparatively inexpensive, so extrusion wins clearly at low and medium volumes. Die casting requires a more expensive mould, so it becomes competitive only once volume amortizes the tool.
The practical implication: if you need 500 pieces of a straight-fin heat sink, extrusion. If you need 50,000 pieces of a housing with integrated mounting bosses, die casting — but only if the geometry justifies the tooling.
Geometry capability
Extrusion handles:
- - Long, straight fin arrays with consistent fin thickness and pitch
- - Constant cross-sections of essentially any profile
- - Lengths cut to specification
- - High aspect ratio fins
Extrusion cannot handle:
- - Holes or slots running perpendicular to the extrusion axis
- - Internal cavities closed in cross-section
- - Varying cross-section along the length
- - Complex three-dimensional contours
Die casting handles:
- - Complex housings with integrated bosses, ribs and mounting features
- - Non-uniform wall thickness (within limits)
- - Curved and organic shapes
- - Features on multiple faces that would require separate machining operations on an extrusion
Die casting cannot handle:
- - Very thin, high aspect ratio fins
- - Very long parts
- - Sections thinner than roughly 1 mm (alloy and geometry dependent)
Thermal performance
For heat transfer, extrusion generally produces better results.
The reason is metallurgical. Extruded aluminium has a dense, directionally consistent grain structure with essentially no internal voids. Die castings inevitably contain some porosity, and porosity reduces effective thermal conductivity in the affected region.
For a heat sink whose entire purpose is conducting heat away from a device, that matters. This is why high-performance forced-air heat sinks are almost always extruded, and why die cast heat sinks tend to be found in lower-power or appearance-driven applications.
That said, if your design requires complex geometry that extrusion cannot produce, a well-designed die cast heat sink with adequate cross-section will outperform an extruded heat sink that does not fit your envelope. Geometry beats material properties when the geometry is the constraint.
Surface finish and appearance
Both processes accept the full range of finishes we offer — anodizing, brushing, polishing, sandblasting, coating, laser marking and silkscreen printing.
One difference worth noting: die castings may show small surface imperfections (flow marks, minor porosity at the surface) that become more visible after polishing or bright anodizing. If a defect-free cosmetic surface is critical, extrusion or a machined-from-solid approach may be the safer choice.
A decision shortcut
Ask these four questions in order:
- 1. Is the geometry achievable by extrusion? If the cross-section is constant along the length, extrusion is almost always cheaper.
- 2. What is the annual volume? Below roughly 10,000 pieces, extrusion's low tooling cost usually dominates. Above that, evaluate casting seriously.
- 3. Is thermal performance critical? If yes, prefer extrusion for better material density.
- 4. Do you need integrated 3D features? If yes, casting avoids secondary machining operations and may win on total cost despite higher tooling.
The hybrid answer
The two processes are not mutually exclusive, and the best solution sometimes uses both: an extruded heat sink body with a die cast mounting bracket, or a die cast housing with an extruded fin insert.
Because we run extrusion, die casting, CNC, stamping and surface treatment in one plant, we can evaluate the hybrid option — which is difficult when your extrusion supplier and your casting supplier have no reason to talk to each other.
Not sure which process your part needs? Send your drawing or 3D model to [email protected] and we will recommend the process with the lowest total cost for your volume and geometry.
Keywords: extruded heat sink vs die cast, aluminium extrusion vs die casting, heat sink manufacturing process selection, custom heat sink design guide, aluminium heat sink supplier